
Blog · CIM UPC
Wire electrical discharge machining (wire EDM) is a machining process used to make high-precision cuts in conductive materials. Instead of cutting with a tool that applies force to the part, the material is eroded by electrical discharges. This makes it especially useful when a part is very hard, has considerable thickness or needs very fine details. Fundació Centre CIM (CIM UPC), an entity belonging to the Universitat Politècnica de Catalunya – BarcelonaTech, offers it as part of its CNC machining service.
How it works: sparks that melt the material
The process relies on electrical discharges jumping between the electrode and the workpiece. It is a thermoelectric process: the sparks act as a localised heat source that melts the material of the part and causes it to erode.
Deionised water is used during the process and has three functions: it promotes the discharge and therefore the quality of the sparks; it cools the eroded material; and it removes the detached material.
Advantages
- It can work with conductive materials of significant thickness.
- The electrode does not need to be machined beforehand.
- It is a high-precision process, with controlled variable angularity.
- It delivers consistent results: the same part can be reproduced time and again.
- Complex shapes can be achieved.
- Previously hardened materials can be machined.
When to use wire EDM
Wire EDM is especially suitable for cutting extremely hard materials and parts without mechanical stress, and for very thick metal parts that could not be cut with laser or water, when the aim is precision rather than productivity, as it is a slow process.
It is also the right technology for very small parts, such as injector pins or needles for medical use; for parts with very thin walls; for cutting small radii; and for cutting stacked materials without the need for clamping supports.
CIM UPC’s ONA FIL machine
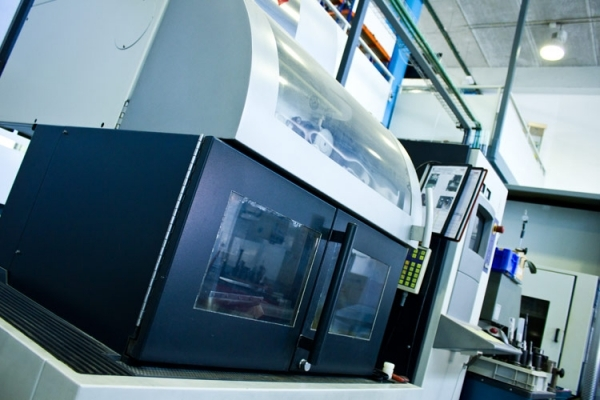
The centre has an ONA FIL machine that can manufacture metal tools and prototypes with a high level of precision and quality surface finishes, and reduce machining time for parts made of conductive materials with great thickness or density. It can also be used to create textures on metal surfaces, which makes it ideal for manufacturing plastic injection moulding tools, the main field of application for this process. Its main features are:
- Number of axes: 4.
- Potential difference: 100–250 V.
- Maximum cutting speed: 240 mm/min.
- Maximum part weight: 500 kg.
- Wire diameter: 0.1–0.3 mm.
Part of a complete machining service
Wire EDM is part of CIM UPC’s CNC machining service, which manufactures metal and plastic components with ISO-certified dimensional quality, and is complemented by the CNC machining centres and the pre-series service. Interested companies can find out more about wire EDM or get in touch with the centre.